Efficient Distillation System Manufactures in India | TOPSE
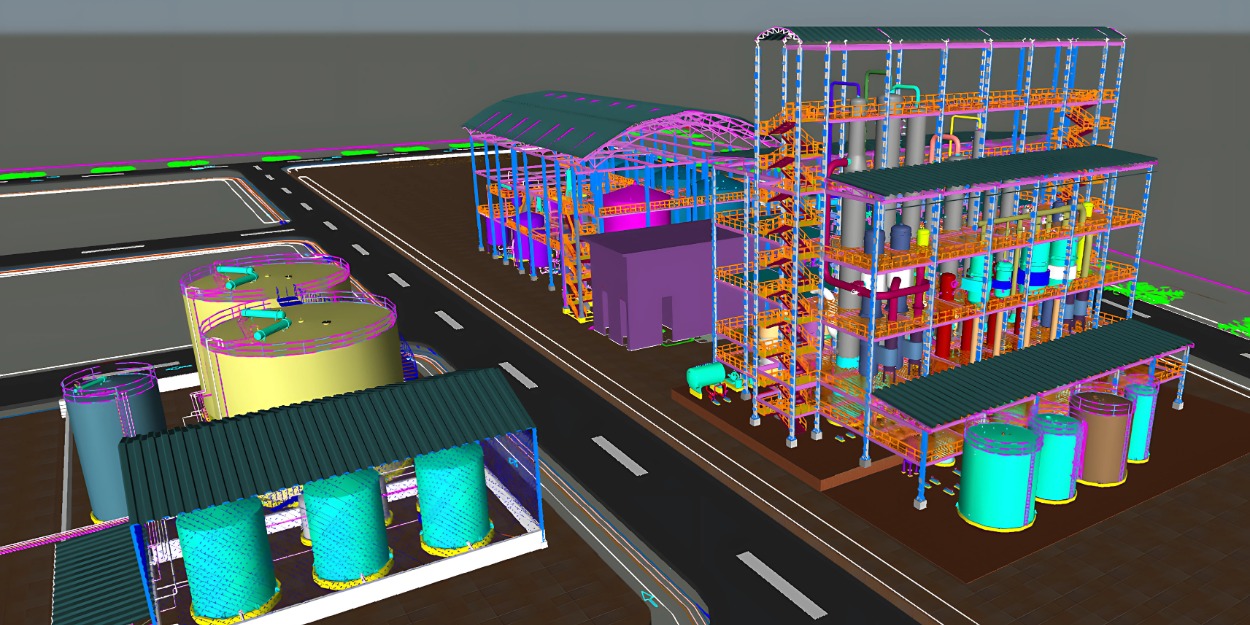
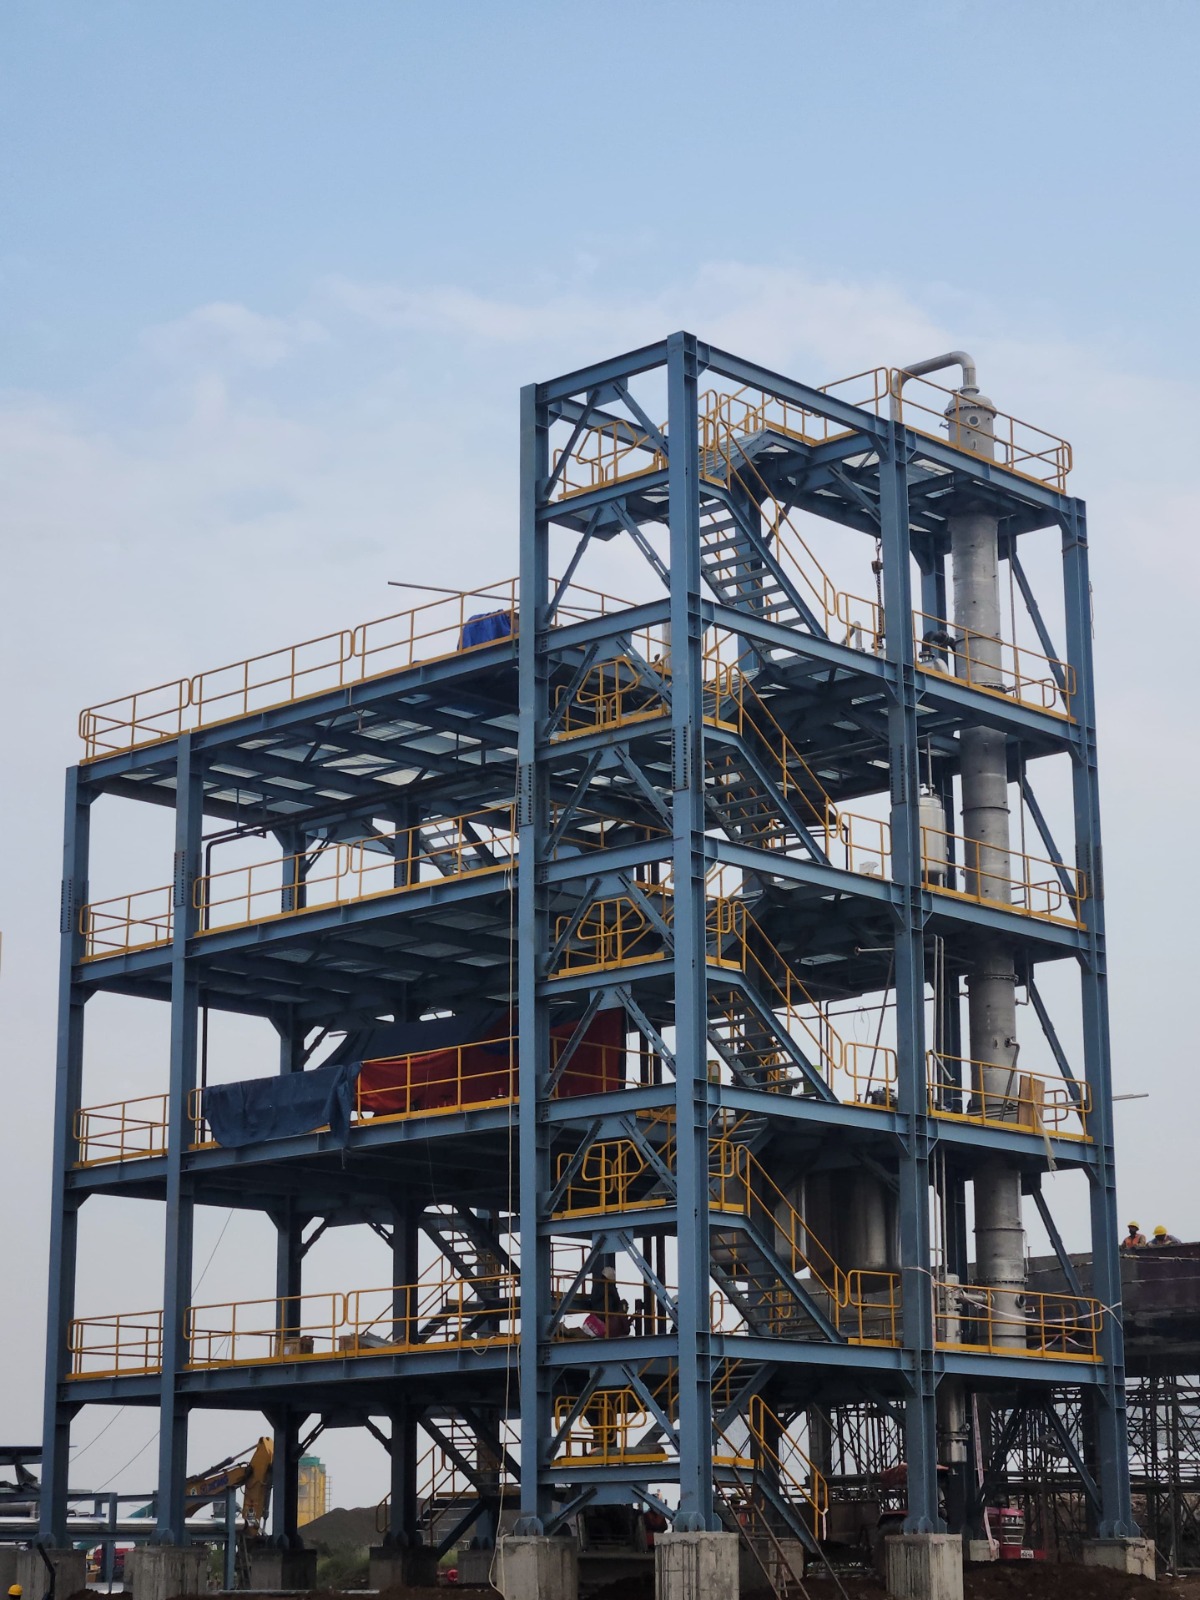
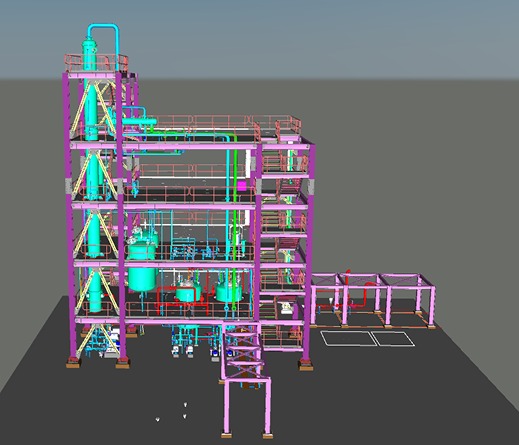
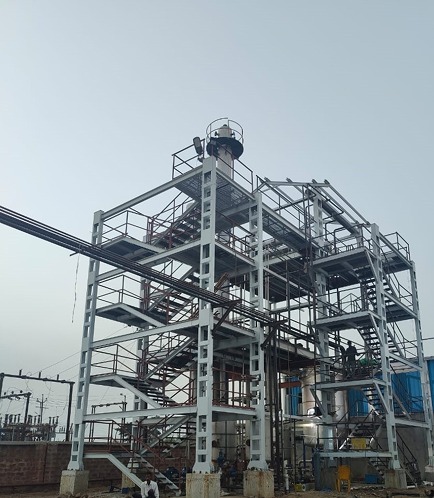
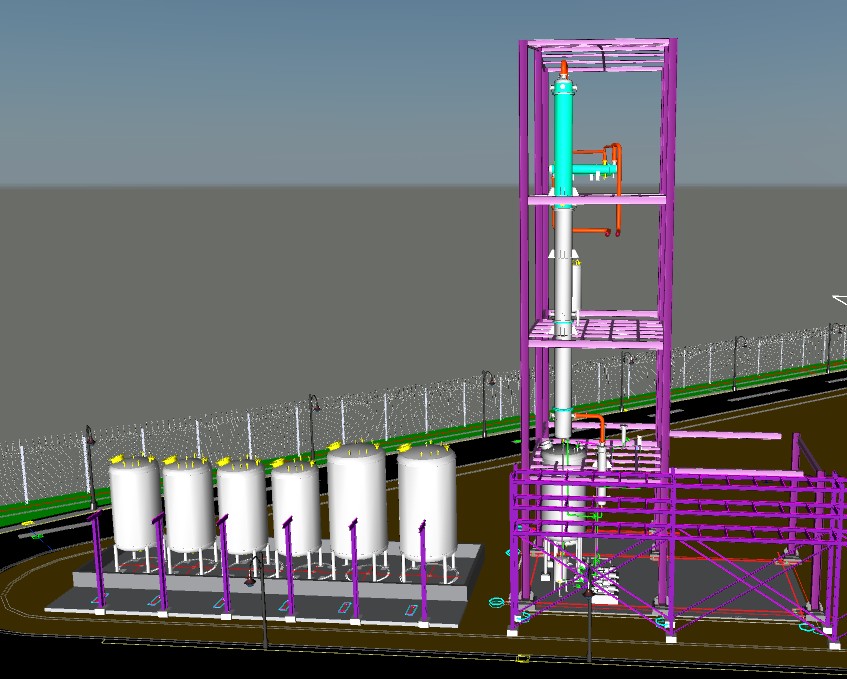
The solvent recovery system from a leading Distillation Manufacturer in India uses a multi-stage distillation approach to recover solvents from waste streams. By leveraging differences in boiling points between solvents and contaminants, the solution is heated to vaporize the mixture, then vapors are condensed into separate liquid fractions across different tanks.
TOPSE’s offerings as a trusted Distillation Manufacturer in India
Multi-component distillation system
Multi-stream distillation system
Azeotropic distillation system
Vacuum distillation system
Reactive distillation system
Extractive distillation system
Solvent dehydration via molecular sieve (PSA & TSA)
Solvent dehydration via molecular sieve (PSA & TSA)
Capacities: Pilot scale to commercial scale
Solvent Recovery Unit
As a reputed Distillation Manufacturer in India, we engineer our Solvent Recovery Unit (SRU) to reclaim and purify solvents from industrial processes. This helps reduce waste, lower operating costs, and supports environmental sustainability.
Key benefits of SRU
Energy-Efficient
Integrated advanced heat recovery systems to lower energy usage and operational cost
Optimized & Precise Design
Engineered for utmost purity and maximum recovery efficiency
Multi-Stream Design
Can handle multiple solvent streams in campaign mode
Safety Systems
Equipped with pressure relief valves, temperature controllers, emergency shutdown systems
Technical Specifications
1. Separation Technology
Continuous and batch distillation columns
Vacuum Distillation
Steam Stripping.
Molecular sieve dehydration (Pressure Swing & Temperature Swing Adsorption)
Membrane pervaporation
2. Types of compounds handled
Alcohols
Aldehydes & Ketones
Acids, Ethers & Esters
Hydrocarbons
3. Plant Capacity and Product Recovery
Industrial scale: 5 KLD up to 2400 KLD
Pilot scale: 500 L/day up to 5 KLD
Product recovery: Up to 99.5%
4. Customization Options: As a leading Distillation Manufacturer in India, we offer customization based on: